





Introducing our revolutionary Industrial Floor Covering System – a superior solution that outperforms all others. This cutting-edge floor covering is built to withstand rigorous conditions, offering unparalleled durability, unique shapes, and a host of benefits.
Product Details
1. Extreme Durability: Our floor covering system is designed to resist wear and tear, making it highly resilient against mechanical, thermal, and chemical loads. Its special shape, thickness, and joint configuration ensure maximum resistance and longevity.
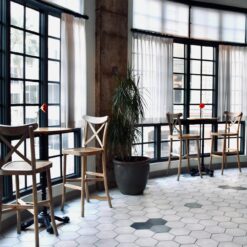
2. Special Shape for Versatility: The hexagonal tiles’ unique design allows for steeper slopes without the need for additional gears, making it suitable for all kinds of traffic and industrial environments. This contributes to enhanced hygiene by efficiently channeling water and chemicals away from the surface.
3. No Joint Worries: The absence of joints in the floor and the short edges of the hexagonal tiles ensure that heavy loads, even from small wheels, are distributed evenly and absorbed with the utmost robustness.
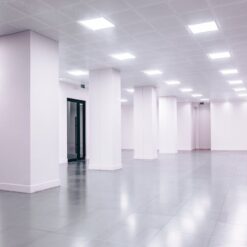
4. Monolithic Appearance and Decorativeity: The Vibrated Ceramic Flooring System provides a seamless, monolithic appearance that enhances the aesthetics of any space. Its decorative nature adds elegance to industrial environments.
5. Hygienic and Easy to Clean: The non-threaded, straight floor surface achieved by narrow joints (1.5-2 mm) offers a homogeneous floor with no down oscillations in the joints, maximizing flatness and ease of cleaning.
6. Tailored Slip Resistance: The hexagonal tiles are available in various anti-slip standards, catering to different operational needs. They offer exceptional slip resistance, especially on wet and greasy floors, ensuring occupational safety.
This Industrial Floor Covering System is a game-changer for industrial and commercial spaces. Its unbeatable combination of strength, aesthetics, and functionality sets it apart from traditional flooring solutions. Invest in this revolutionary system and elevate your floor’s performance and appearance to new heights. Experience the future of industrial flooring today.
Key Features:
1. Industrial-Grade Durability: Our ceramic flooring porcelain tiles are specially formulated to endure the most demanding industrial settings. They are resistant to heavy impacts, abrasion, chemicals, and extreme temperatures, ensuring longevity and reliability even in high-traffic areas.
2. Non-Slip Surface: Safety is a top priority, and these tiles are engineered with a non-slip surface, providing excellent traction even in wet or oily conditions. This feature is critical for industries where safety is paramount, such as manufacturing plants, warehouses, and loading docks.
3. Low Maintenance: With these ceramic tiles, maintenance becomes a breeze. Their non-porous surface repels dirt, grime, and stains, making them easy to clean and maintain over time. This low-maintenance quality ensures a hygienic environment and reduces overall operational costs.
4. Versatility in Design: While engineered for industrial applications, these porcelain tiles also boast an aesthetically pleasing design. They come in a variety of colors, patterns, and textures, allowing you to customize your flooring while maintaining a professional and modern appearance.
5. Chemical Resistance: The tiles’ exceptional chemical resistance makes them ideal for industries dealing with harsh chemicals, acids, and alkalis. This feature ensures that the tiles maintain their integrity and appearance, even when exposed to aggressive substances.
Applications:
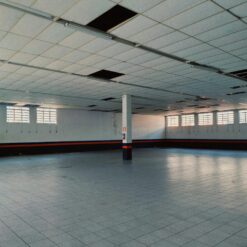
1. Manufacturing Plants: These ceramic tiles are a perfect fit for manufacturing facilities, where heavy machinery, constant foot traffic, and potential chemical spills demand durable, high-performance flooring.
2. Warehouses and Distribution Centers: With their non-slip surface and high-load-bearing capacity, these tiles provide a secure and stable floor surface for efficient movement of goods and equipment.
3. Commercial Kitchens: In busy commercial kitchens, the resistance to stains, chemicals, and moisture is crucial for maintaining a hygienic and safe working environment.
4. Laboratories: The chemical-resistant properties make these tiles suitable for laboratories where spills and exposure to hazardous substances are common.
5. Automotive Workshops: The tiles’ ability to withstand oil, grease, and heavy impacts makes them a valuable addition to automotive workshops and service centers.
6. Retail Spaces: The versatile design options allow these tiles to be used in retail spaces, adding a touch of elegance while providing the durability necessary for high foot traffic.
Invest in our Technical Industrial Ceramic Flooring Porcelain Tiles today, and experience the perfect blend of strength, functionality, and style. Revolutionize your industrial and commercial spaces with a flooring solution that exceeds expectations and stands the test of time.
Technical values:
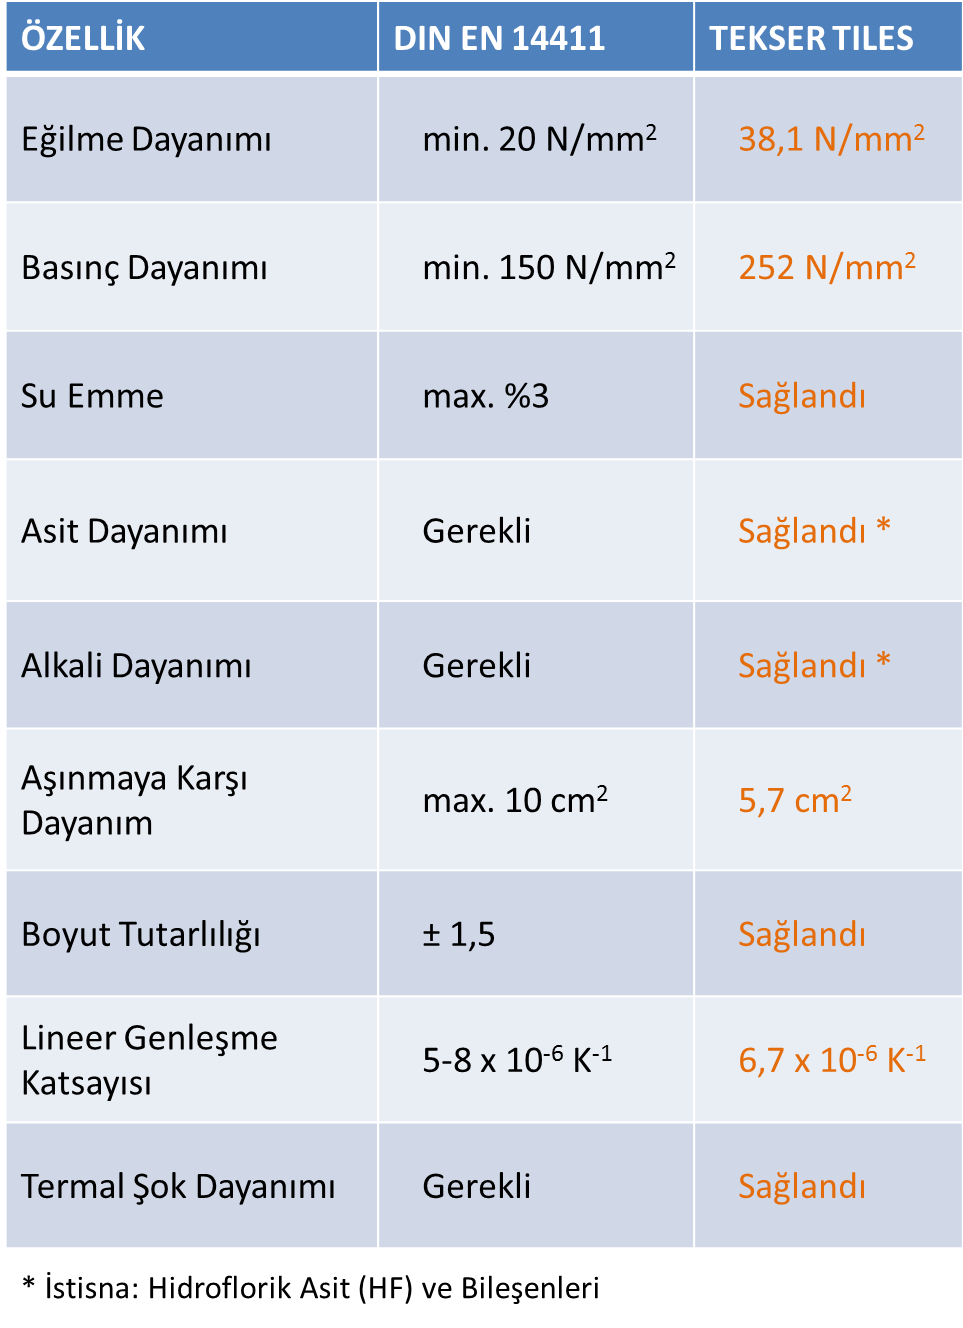
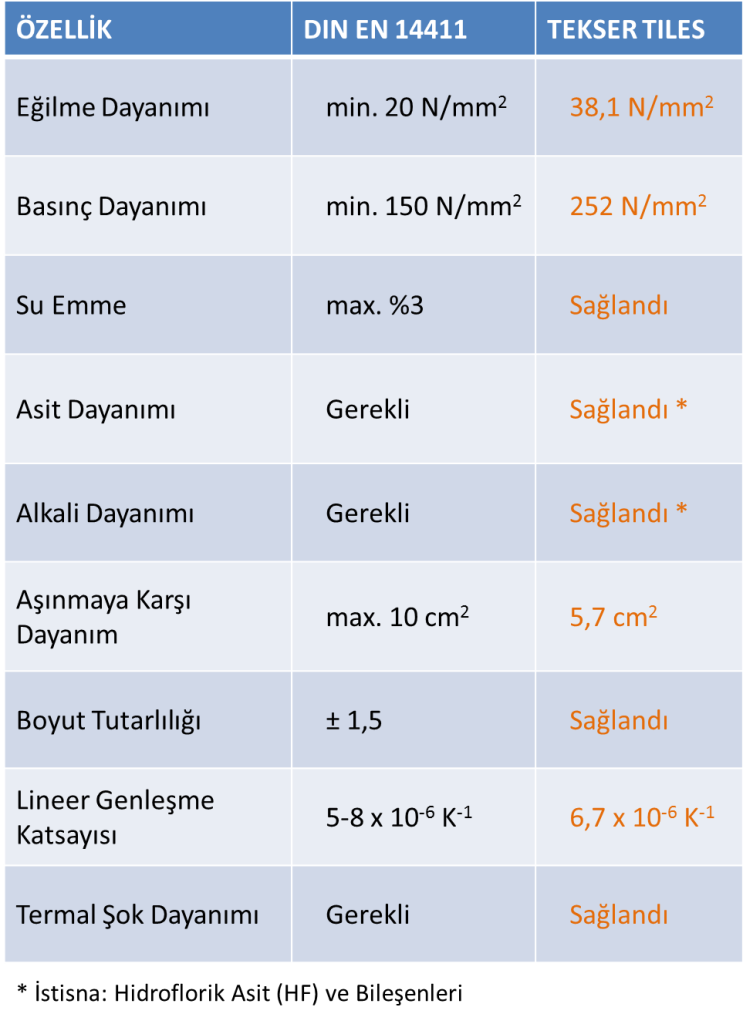
Tested according to DIN EN ISO 10545 Section 1-16 Hexagon porcelain comply in all tested properties with the requirements of material Norm DIN EN 14441, Section G, Group B I and UGL.”
Tarek, Palestine –
After using it for a while, I’m convinced this product is a game-changer! Al Hariri Group’s food production machine has proven its worth in my operations.
Bilal, Yemen –
This product has promise but requires refinement. While it’s a good product overall, it falls a bit short of the initial expectations I had.